- All
- Product Name
- Product Keyword
- Product Model
- Product Summary
- Product Description
- Multi Field Search
Views: 0 Author: Site Editor Publish Time: 2026-10-17 Origin: Site


Packaging has evolved far beyond mere product protection in modern manufacturing. Today, forward-thinking brands treat this outer layer as a primary, shelf-ready brand asset. You must capture consumer attention immediately on crowded retail shelves. However, companies constantly struggle to balance packaging costs, sustainability goals, and high visual impact. Adding secondary paper labels or bulky cardboard boxes simply increases material expenses. It also creates unwanted complexity in your supply chain. You need a streamlined, efficient approach to secure and market products simultaneously. This guide provides a clear, engineering-focused framework for evaluating your packaging line. We outline procurement strategies to help you make informed decisions. You will learn if transitioning to a printed wrap makes financial and operational sense for your facility. We will explore printing mechanics, advanced material choices, and potential risks. By understanding these technical variables, you can optimize your packaging process effectively.
Replacing blank film and secondary labels with printed film can reduce total packaging footprint and simplify the supply chain.
**Printed POF shrink film** is the standard for retail applications due to its FDA-compliant safety, high clarity, and lack of toxic off-gassing.
Achieving high-fidelity branding requires precise distortion calculations prior to **printing shrink film** to ensure graphics render correctly post-heat tunnel.
Upgrading to **8-color printed shrink film** enables exact Pantone matching and complex photographic imagery but requires analyzing Minimum Order Quantities (MOQs) and lead times.
Applying ink directly to a polymer film before it wraps your product requires immense precision. Manufacturers typically rely on two primary methods: flexographic or rotogravure presses. Flexographic printing uses flexible photopolymer plates wrapped around rotating cylinders. It deposits ink onto the flexible substrate in rapid succession. Rotogravure uses engraved metal cylinders for even higher volume, highly detailed runs. You then roll the printed material for use on automated wrapping lines. This direct-to-film process completely eliminates the need for separate sticker applications.
The primary technical challenge lies in managing graphic distortion. Engineers must calculate the exact shrink ratio of the film before any ink touches the surface. They analyze the machine direction (MD) versus the transverse direction (TD). Mastering printing shrink film demands advanced prepress 3D modeling. Designers pre-distort the image deliberately on the digital file. They stretch logos and text based on the specific contour of the product. When the package passes through the heat tunnel, the graphics shrink into perfect proportion.
Film surface treatment is also mandatory for success. Polymer films naturally resist ink adhesion due to their low surface energy. Manufacturers apply a corona treatment to the material surface prior to printing. This high-voltage electrical discharge modifies the molecular structure of the film. It creates microscopic abrasions that allow inks to bond securely.
Common Mistake: Skipping or under-treating the film surface. Without proper corona treatment, the printed design will flake, scratch, or rub off entirely during the intense shrinking phase inside the heat tunnel.
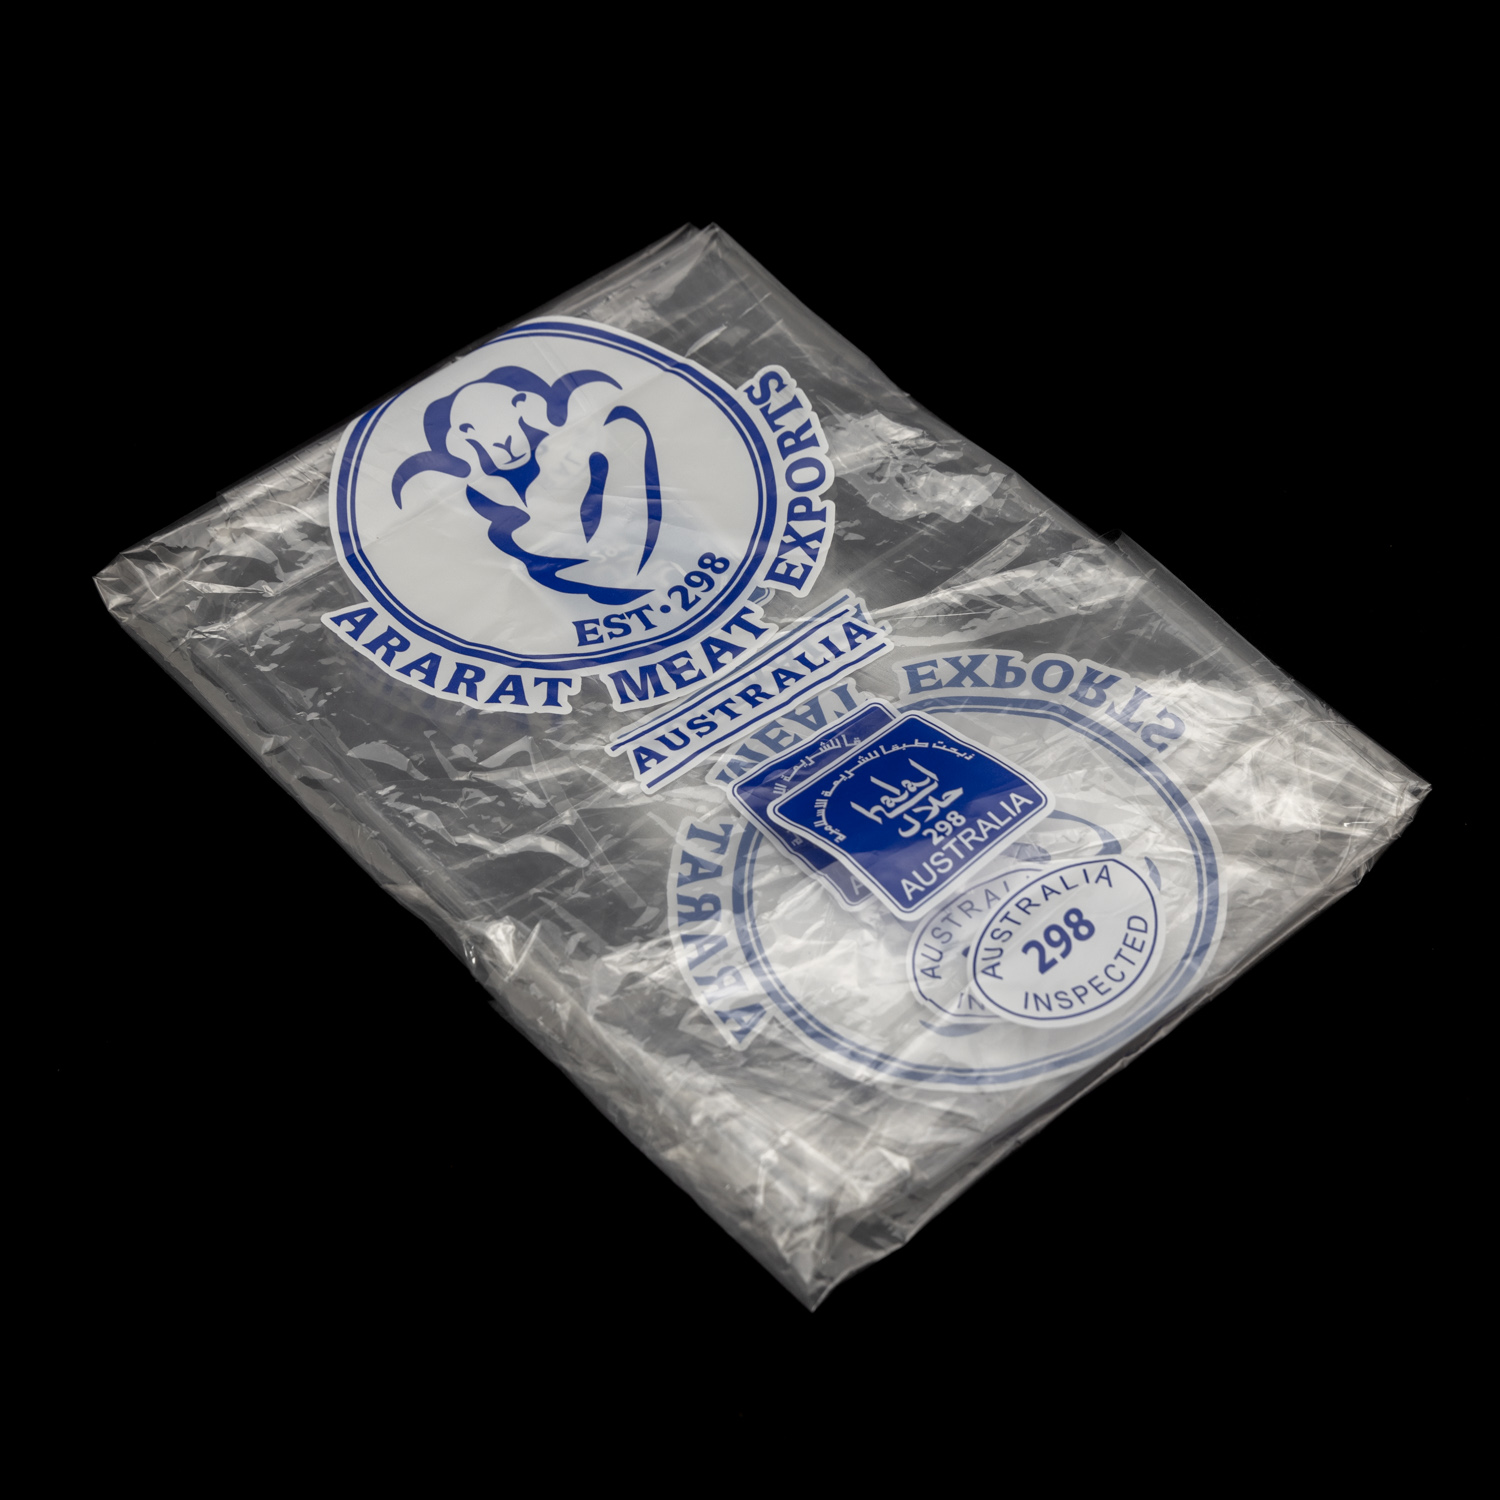
Moving away from unprinted films offers distinct, measurable financial advantages. You must compare the total unit cost comprehensively. Consider the combined price of clear wrap, adhesive labels, chipboard cartons, and the glue required to hold them together. Then, compare that combined expense to a single roll of custom printed shrink film. The printed roll carries a higher upfront material cost per foot. However, it significantly reduces manual labor and secondary material usage. You streamline operations by eliminating label applicators and carton erectors from your facility floor.
This approach also unlocks powerful 360-degree branding opportunities. Multipacks like bottled water, canned energy drinks, or bundled cosmetics benefit immensely. You utilize the entire surface area of the package. It provides ample space for vibrant marketing graphics visible from any angle. You can also easily fit mandatory nutritional information, barcodes, and recycling instructions without cluttering the primary display panel.
Furthermore, printed graphics enhance tamper-evident security. If someone opens or compromises the package, the printed design distorts irreparably. The continuous graphic breaks, making it obvious that tampering occurred. This provides an immediate, visible layer of product security. Consumers instantly recognize untampered goods. Building this lasting brand trust is crucial in the food, beverage, and pharmaceutical sectors.
Choosing the right polymer formulation dictates your packaging success. Polyolefin (POF) represents the modern standard for retail display environments.
POF boasts superior tear resistance, exceptional puncture strength, and high clarity. It complies fully with strict FDA regulations for direct food contact. Historically, many brands used Polyvinyl Chloride (PVC) for retail packaging. However, the industry has largely phased out PVC. PVC releases toxic chloride gas emissions when exposed to heat sealing wires. These emissions corrode machinery and pose health risks to machine operators. POF offers a safer, cleaner, and more robust alternative for your facility.
You must also differentiate POF from Polyethylene (PE). PE serves excellently for heavy-duty transit. You often see thick PE used for bullseye wraps on heavy beverage trays or industrial pallets. However, POF remains the definitive choice for premium retail displays. It requires lower shrink temperatures, which protects heat-sensitive products. It also delivers a crystal-clear, high-gloss finish that enhances ink vibrancy.
Sustainability matters to modern consumers and corporate stakeholders alike. We must address recyclability transparently to avoid greenwashing. While POF is fully recyclable, it usually requires specialized drop-off streams. Consumers typically must return it to grocery store collection bins alongside PE grocery bags. Proper disposal ensures your sustainability claims remain authentic. Utilizing printed POF shrink film meets both high-performance marketing and environmental safety needs when managed correctly.
Material Comparison Chart for Packaging Films
Material Type | Retail Clarity | Food Safety (FDA) | Heat Tunnel Odor | Ideal Application Use Case |
|---|---|---|---|---|
Polyolefin (POF) | Excellent / High Gloss | Yes | None | Premium retail display, multipacks, direct food contact |
Polyethylene (PE) | Low / Hazy | Varies by grade | None | Heavy-duty transit, industrial bullseye wrapping |
Polyvinyl Chloride (PVC) | Good | No | High (Toxic Chloride) | Largely phased out due to safety risks |
Brands often demand striking visuals to compete aggressively in retail environments. Advanced printing presses can deliver CMYK base colors plus up to four specific spot colors. They can also apply opaque white underlays behind the design.
Specifying 8-color printed shrink film elevates your package aesthetics dramatically. Let us explore the best application scenarios for this high-end printing capability.
Use this technology when:
Matching strict corporate Pantone colors to maintain brand consistency globally.
Printing high-resolution, appetizing food photography that requires rich, true-to-life color reproduction.
Requiring an opaque white base on clear packaging. This ensures text and barcodes remain perfectly readable against a dark product background.
Avoid this technology when:
Running simple, single-color promotional text or seasonal warning labels.
Using minimalist designs where lower-cost, 2-color printing methods easily suffice.
Operating on extremely tight, last-minute production schedules with no room for prepress delays.
Keep supply chain lead times in mind. Highly complex, multi-color jobs demand precise plate creation for each individual color layer. This initial setup takes time and engineering resources. It can extend your production schedule and affect short-term agility. Plan your inventory replenishments accordingly to avoid stockouts.
Transitioning to Printed Shrink Film requires absolute machine readiness. This material is highly unforgiving of poor machinery setups or outdated equipment.
First, evaluate your heat tunnel consistency. Uneven heat distribution will warp barcodes beyond recognition. It ruins carefully designed branding and distorts nutritional text. You must audit tunnel airflow meticulously. Modern dual-zone heat tunnels provide the best results. Precise temperature controls and adjustable air velocity are strict prerequisites for success.
Second, consider the Coefficient of Friction (COF). Ink fundamentally changes the surface texture of the polymer. The slip characteristics will alter compared to blank film. Procurement teams must verify the COF with the film supplier. It must align seamlessly with your automated wrapper's specific feed mechanics. If the film drags or grips incorrectly, the packaging line will jam, causing costly downtime.
Finally, transparently assess production volume and Minimum Order Quantities (MOQs). Custom print runs necessitate MOQs to justify the press setup time and plate costs. You face a financial barrier for very small batches. Brands must balance the cost of holding printed inventory in a warehouse. Compare this holding cost against the substantial savings achieved through high-volume, continuous print runs.
Best Practices for Implementation:
Audit your existing heat tunnel temperature maps using thermal sensors.
Request printed film samples that mimic your exact artwork coverage.
Run a low-speed test on the wrapping machine to observe COF behavior.
Adjust the sealing jaw temperature, as inked areas may require slightly different heat settings.
Transitioning to a customized wrap balances visual return on investment against technical machine readiness. You can effectively eliminate secondary labels, reduce material waste, and streamline your supply chain. However, you must carefully calculate graphic distortion, audit your heat tunnels, and strategically manage inventory volumes to succeed.
Take action by requesting sample rolls first. Test these samples extensively on your specific heat tunnel equipment. Verify the slip characteristics to prevent automated line jams. Finally, conduct a comprehensive overall financial analysis. Compare your current multi-step packaging process to a streamlined, single-roll solution to determine your true cost savings.
A: No, provided the ink is kept clear of the exact sealing zones, such as lap or fin seals. Manufacturers also use correct slip-additives to maintain structural integrity. The film retains its original tear resistance and tensile strength during the heat application.
A: By utilizing advanced 3D modeling software during the prepress stage. Designers pre-distort the barcode based on the exact geometry of the product and the film's known shrink metrics. Once the package exits the heat tunnel, the barcode shrinks into a perfectly scannable shape.
A: Yes, on a per-roll basis due to inks, printing plates, and machine setup. However, it frequently lowers the overall packaging cost. It completely eliminates the need for secondary boxes, adhesive labels, and the manual labor required to apply them.


